Description
Overview
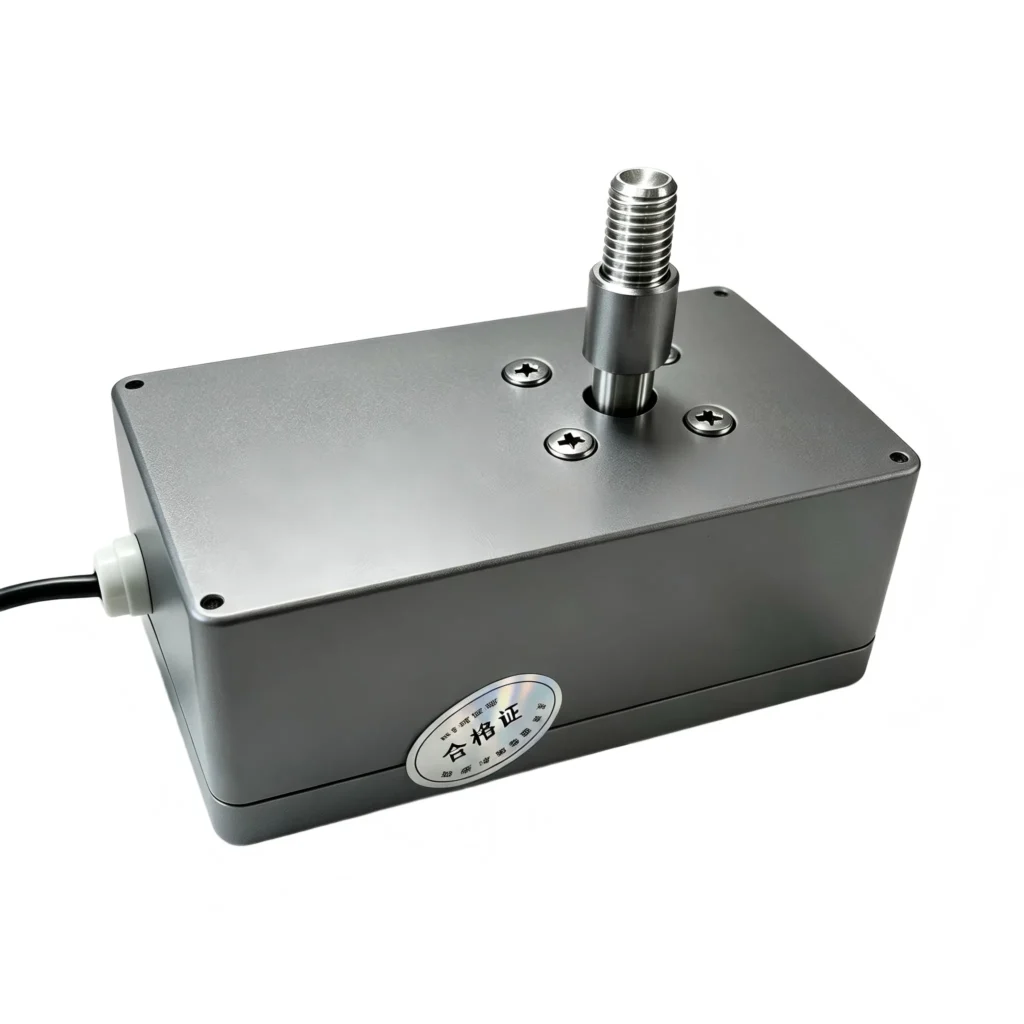
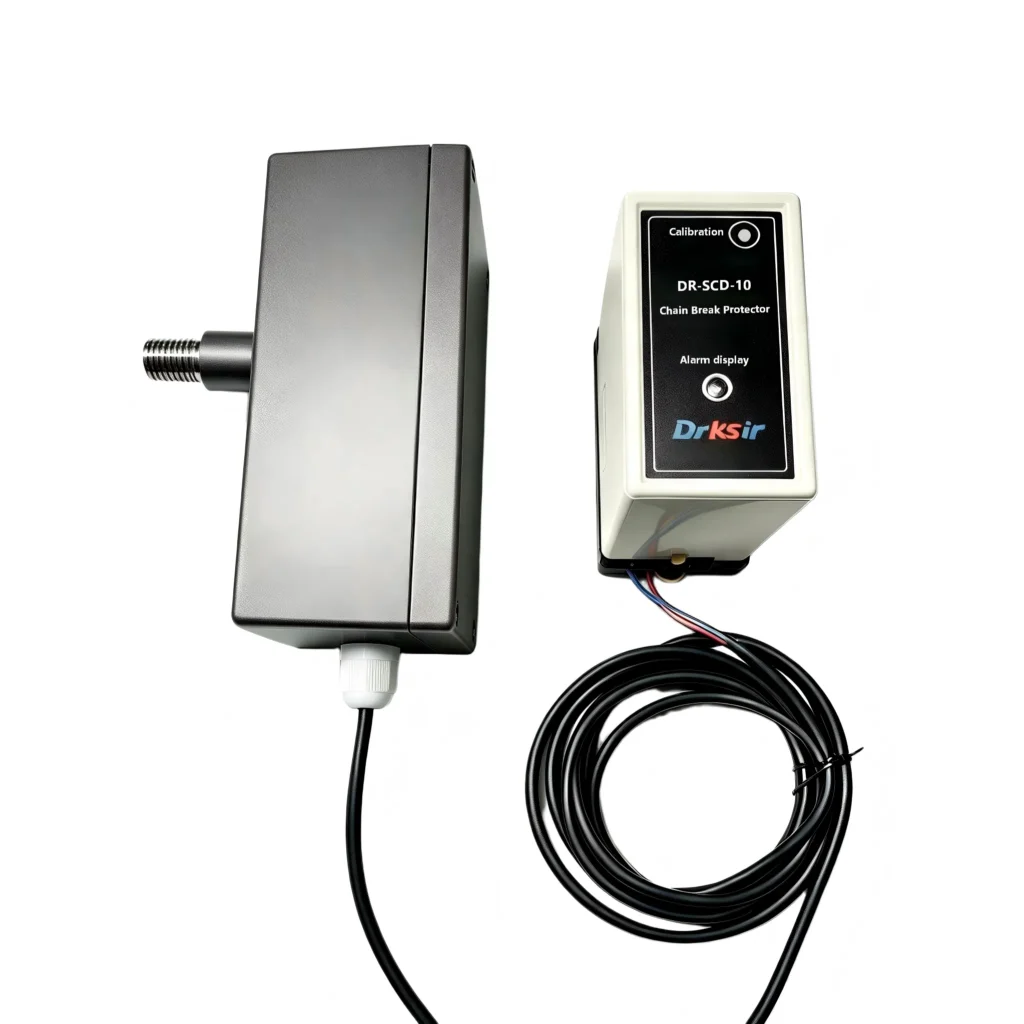
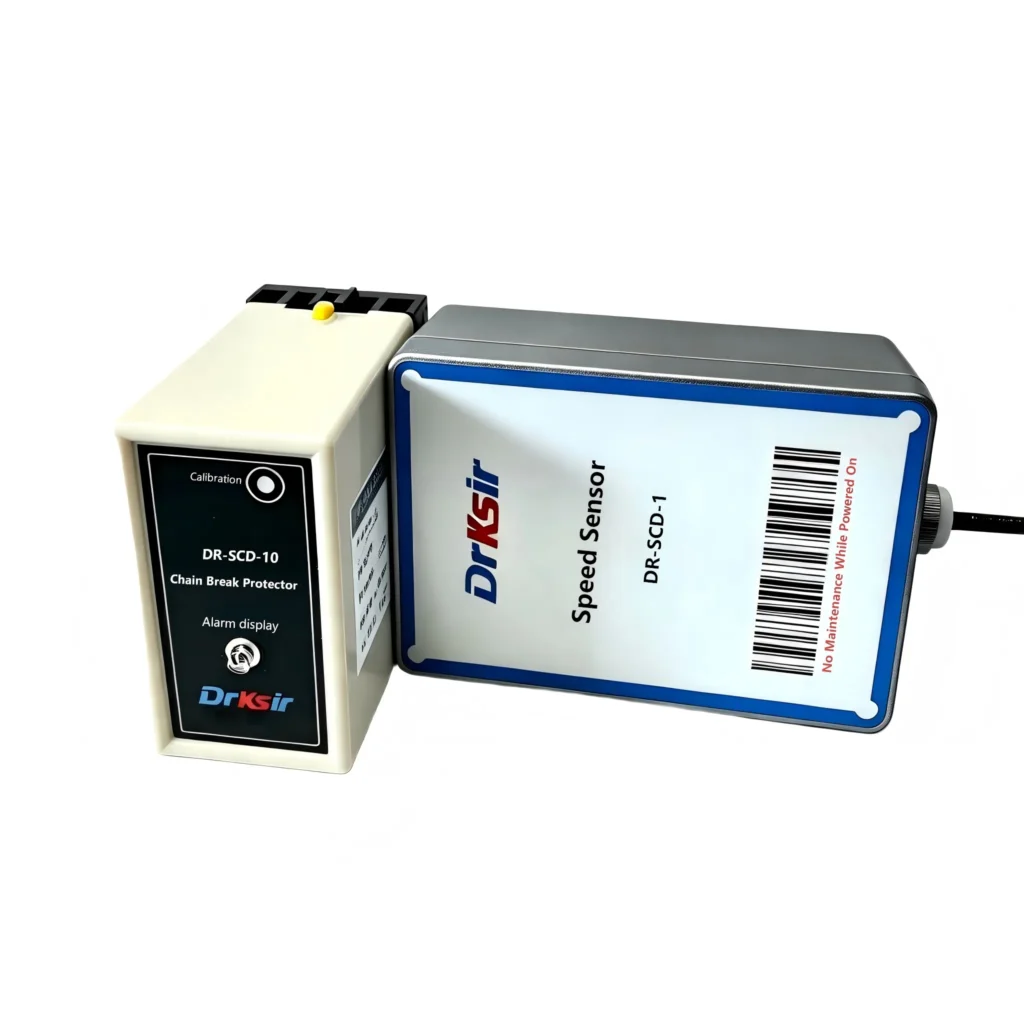
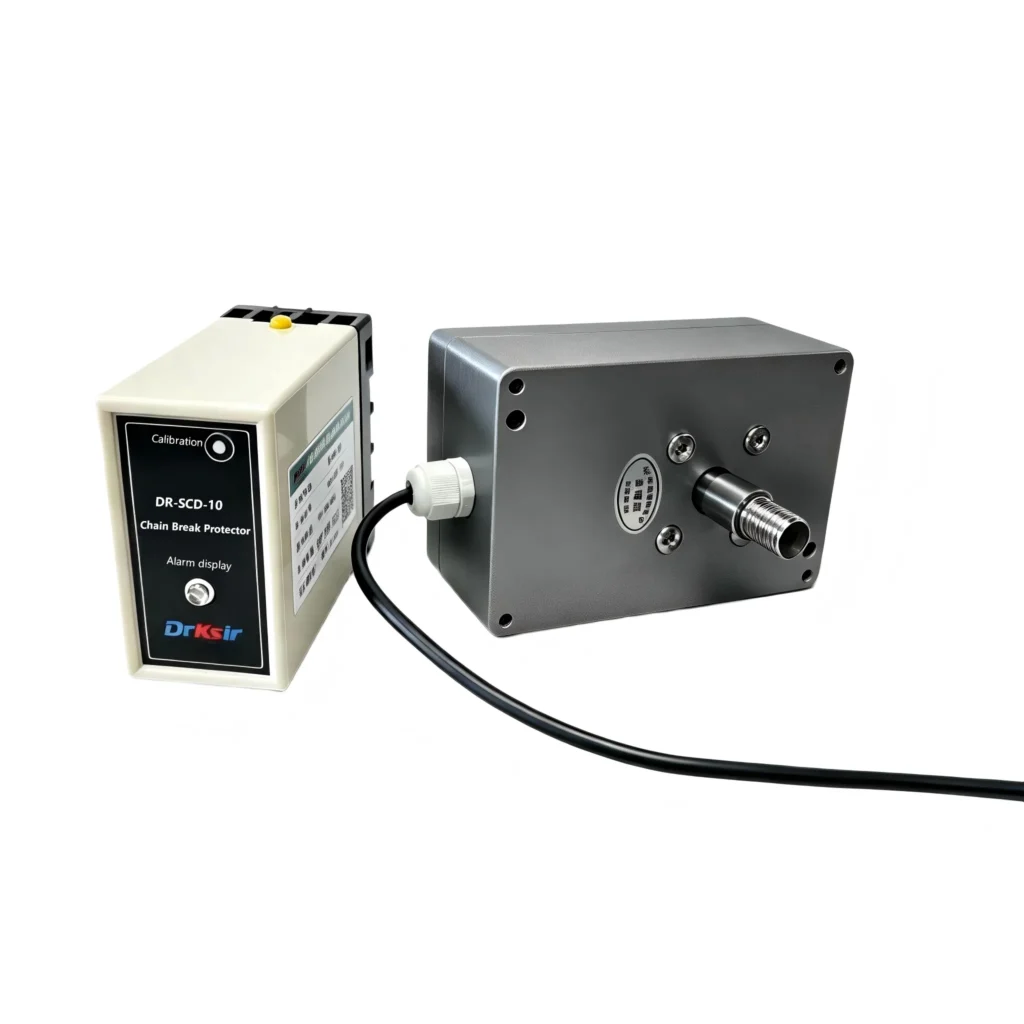
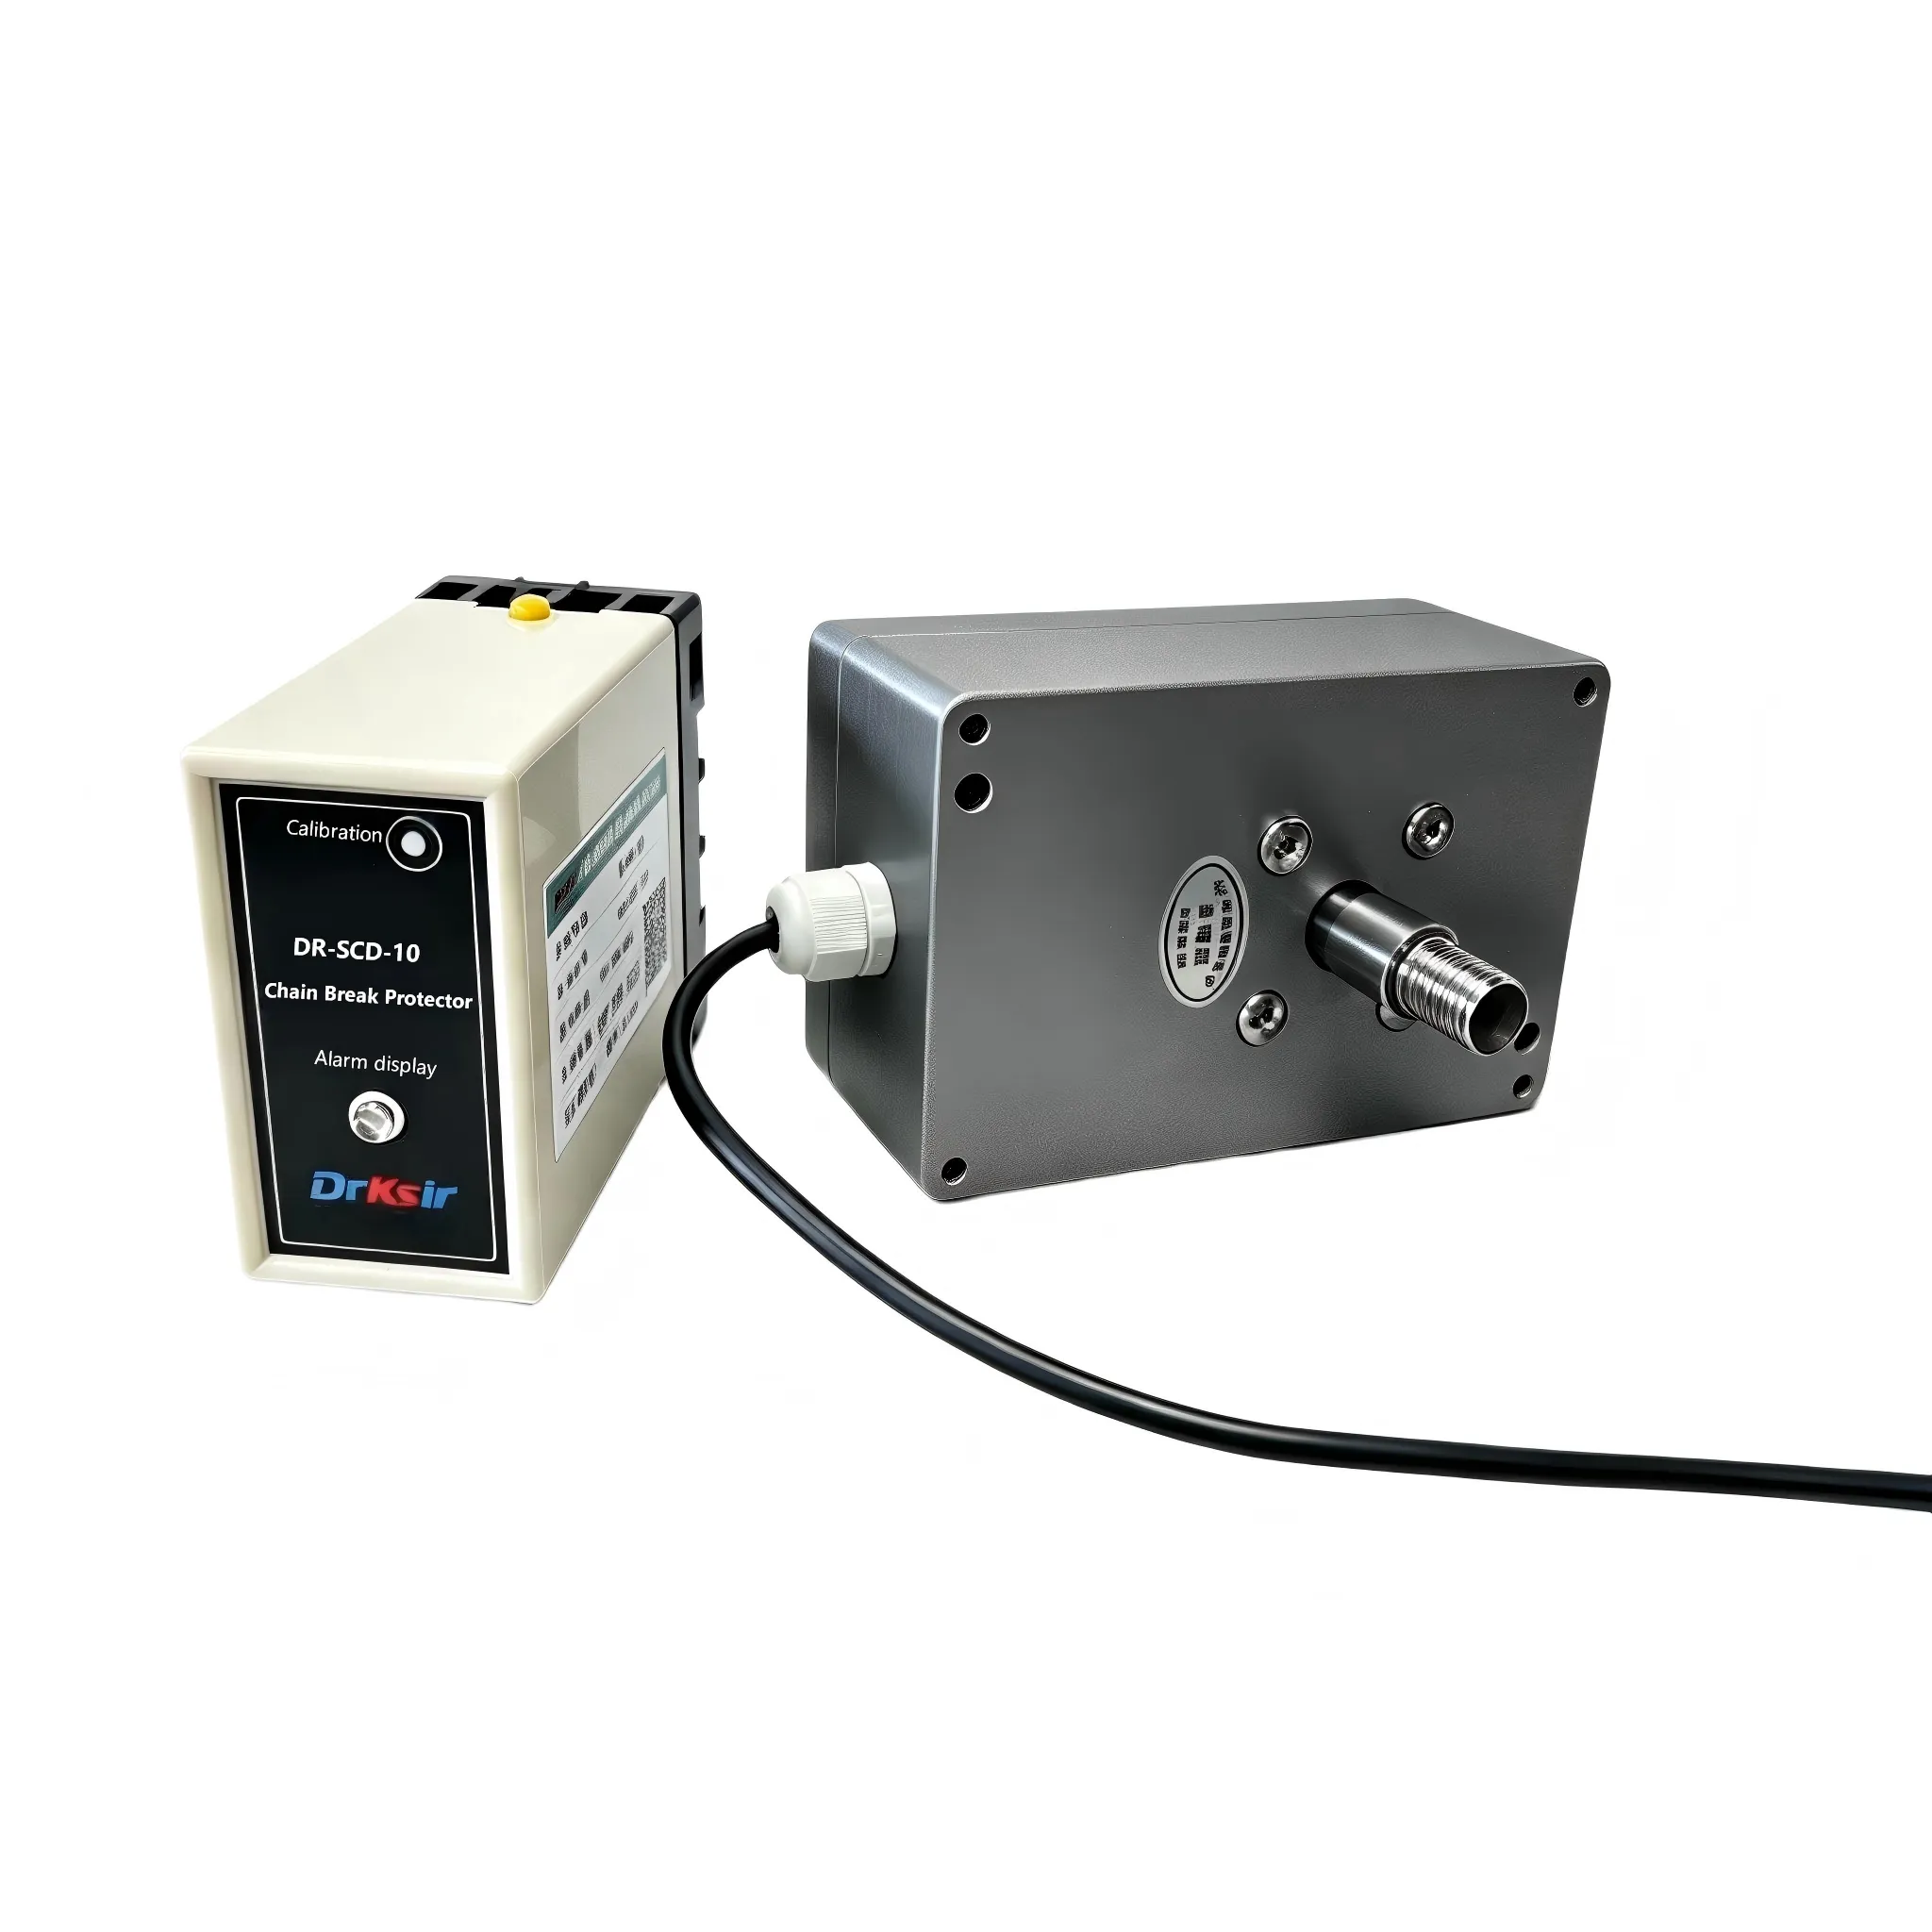
The drksir DR-SCD-10-G is a shaft-speed switch built for scraper (drag-flight) conveyors, where a broken or slipped chain can silently stall the line and cascade into costly downstream damage. It couples to the driven shaft via a threaded sensor screw and trips the relay the moment shaft speed falls below the set threshold — so the drive stops promptly after a chain break, before secondary failures spread.
How It Works
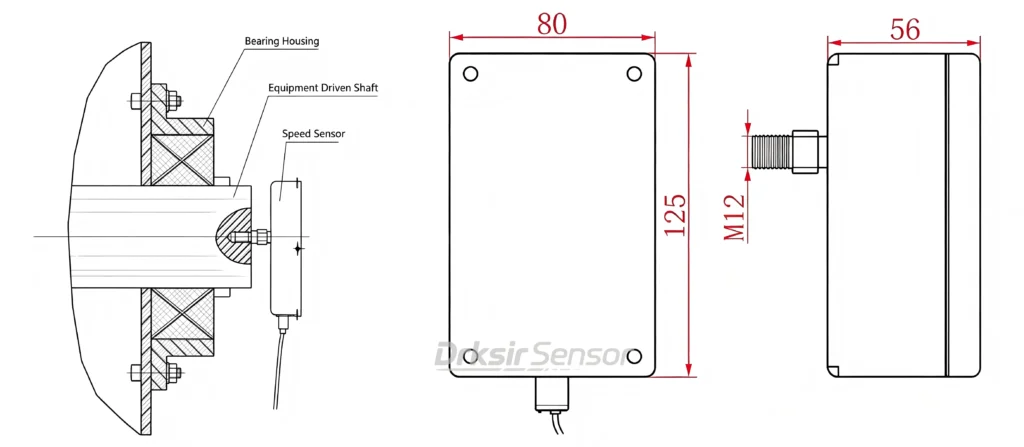
The speed sensor is mounted to the driven shaft through a mechanical screw connection at the shaft end. As the conveyor runs, the driven shaft drives the sensor screw directly, and the controller compares the live pulse signal against a preset threshold — 40 %, 50 %, 60 % or 70 % of the normal running speed (selector switch). When the chain breaks, slips or jams, the shaft slows below the threshold and the protector instantly fires a potential-free relay to cut the driving motor. A sound-light alarm output is also available to alert operators.
Key Features
- Direct mechanical coupling — sensor screw engages the driven shaft center and rotates with it; no slip, no drift in zero-speed detection
- 4 selectable trip thresholds (40 / 50 / 60 / 70 % of normal speed) to match any conveyor
- One-button auto-calibration: hold the Set/Reset button 3 s, the unit learns and stores the normal speed as the threshold automatically (takes 2–300 s)
- 20-second start-up delay bypass — no false trips during motor ramp-up
- Alarm self-lock (DIP switch): latches the alarm after a fault until manually reset, or follows live speed when unlocked
- Status indicator: steady ON = alarm, flashing = calibration mode
- Relay output NO/NC, potential-free contact
Technical Specifications
| Parameter |
DR-SCD-10-G |
| Function |
Zero / under-speed detection (chain break protection) |
| Sensing method |
Shaft-end mechanical coupling — sensor screw driven by monitored shaft |
| Monitored part |
Driven shaft |
| Trip threshold |
40 % / 50 % / 60 % / 70 % of normal speed (selectable) |
| Controller supply |
AC 220 V, 50 Hz (≤3 W) |
| Speed sensor supply |
DC 10–30 V (12 V supplied by controller) |
| Output |
Potential-free relay, AC 220 V / 5 A (also DC 24 V / 5 A) |
| Sensor protection |
IP65 |
| Operating temp. |
−20 ℃ ~ 65 ℃ |
| Relative humidity |
≤95 % (at 25 ℃) |
| Input pulse range |
0.1–10 Hz |
| Duty |
24 h continuous |
| Start-up delay |
20 s |
| Calibration |
One-button auto-learn, 2–300 s |
Installation & Commissioning (shared by SCD-10 family)
- Mount the controller and mechanically couple the speed sensor to the driven shaft through the shaft-end screw connection. Complete wiring and double-check all connections.
- Power on and start the conveyor; wait ~20 s until it reaches stable speed.
- Hold the Set/Reset button 3 s — the red indicator flashes to enter auto-calibration; it turns off when done.
- The unit now monitors continuously; short-press Set/Reset to clear an alarm after a fault.
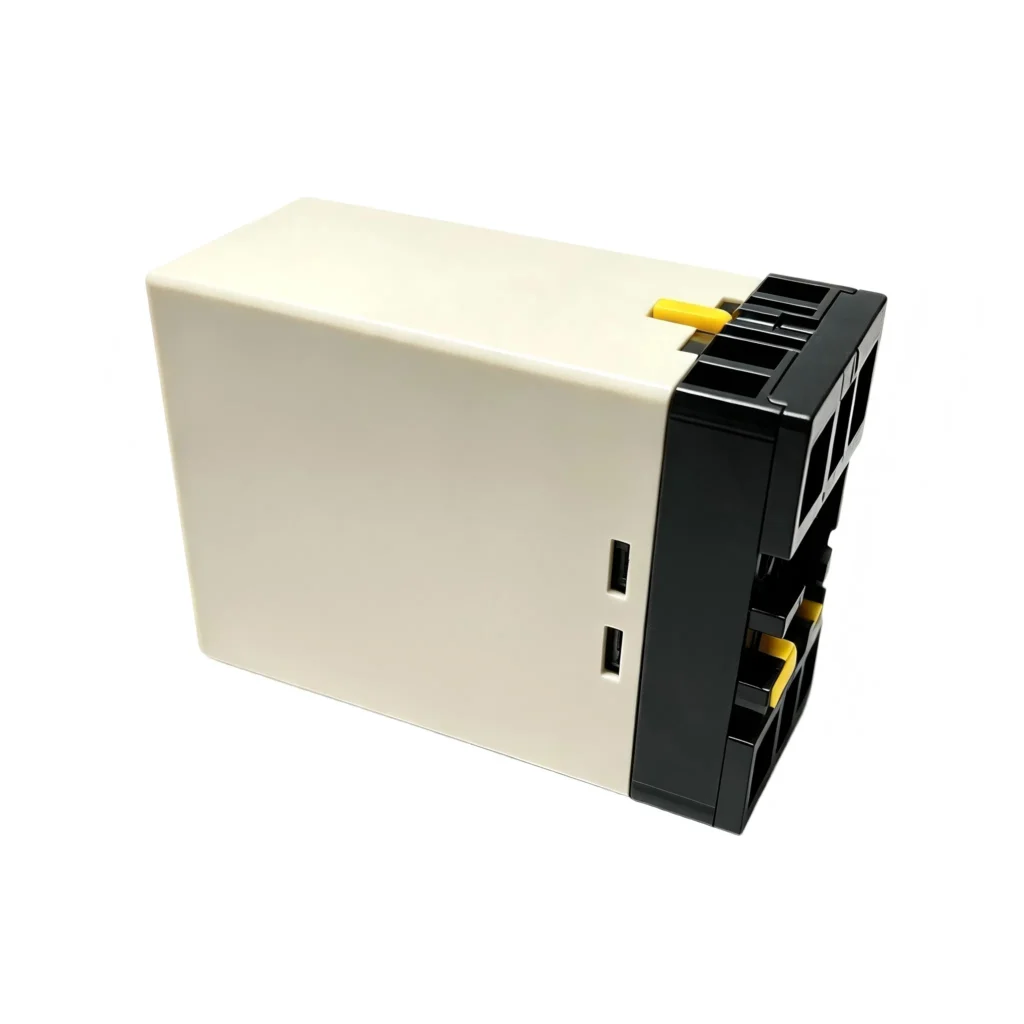
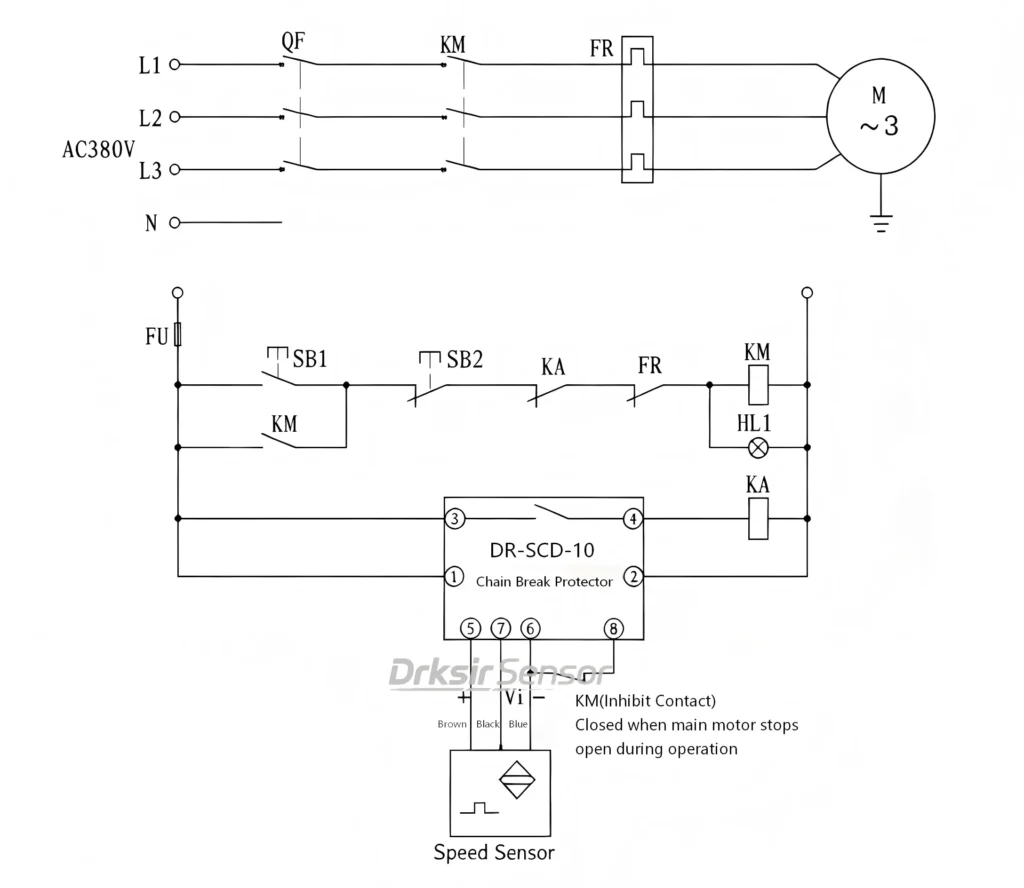
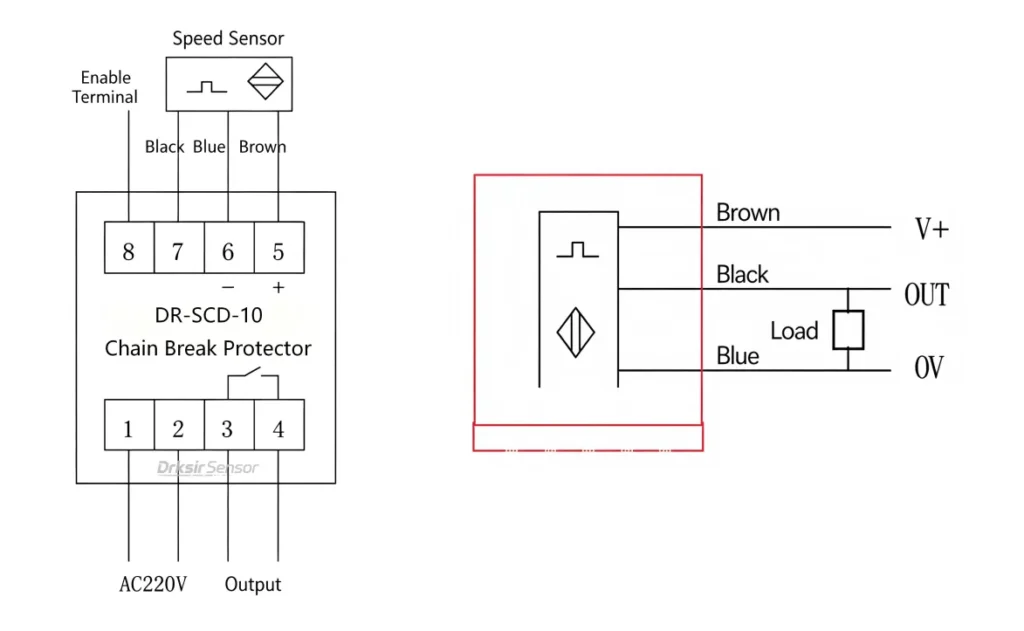
Wiring summary: Controller terminals 1 & 2 → AC 220 V; 3 & 4 → relay output; 5 (+) / 6 (−) / 7 (signal) → speed sensor brown / blue / black wires; terminal 8 → motor contactor auxiliary contact (enable).
Sensor: brown = V+, black = signal out, blue = 0 V.
Where It Fits
- Scraper / drag-flight conveyors in power, biomass and bulk-handling plants
- Ash and slag removal lines
- Any feed system where a chain break means immediate line stoppage
FAQ
Q: How do I know whether I need a zero-speed switch or a chain-skew switch?
A: A zero-speed (under-speed) switch such as the DR-SCD-10 family watches shaft rotation and trips when the chain breaks, slips or the shaft stalls. A chain-skew switch (DR-ICD-20) detects the chain tilting or climbing toward derailment. They solve different failure modes, and on many conveyors both are fitted — the zero-speed switch catches a stopped or slowed line, while the chain-skew switch catches a misaligned one before it jumps the sprocket.
Q: How is the speed sensor mounted to the machine?
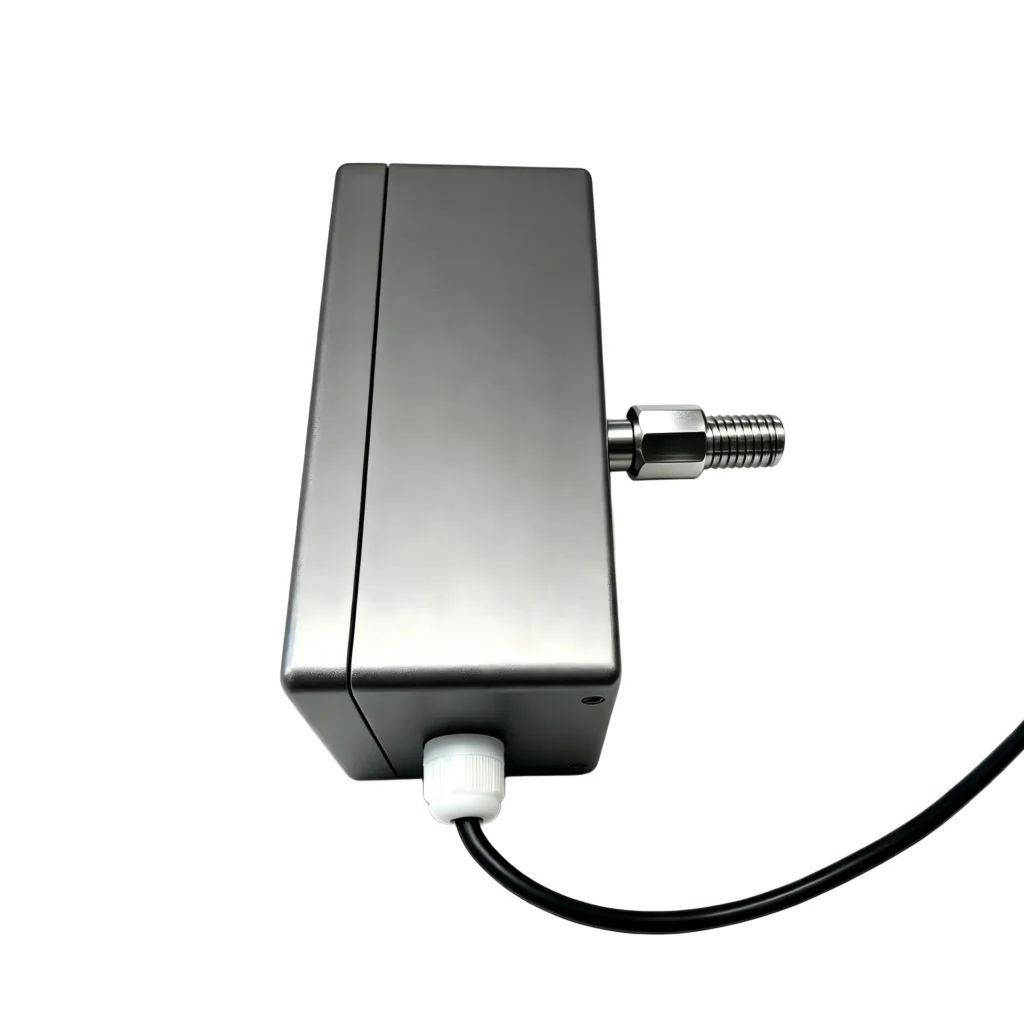
A: The speed sensor couples to the driven shaft through a threaded screw at the shaft end. As the shaft turns it drives the sensor screw directly, so the reading reflects true shaft RPM with no slip. Mounting is mechanical and takes only a few minutes at the shaft end or bearing-housing face.
Q: What power supply and output does it use?
A: The controller runs on AC 220 V, 50 Hz (≤3 W) and supplies 12 V to the speed sensor, which operates on DC 10–30 V. The output is a potential-free relay contact rated AC 220 V / 5 A (also DC 24 V / 5 A) with both NO and NC available, so it drops straight into a motor contactor coil, PLC input or alarm circuit.
Q: How do I set the trip point — and can it self-calibrate?
A: Four thresholds are selectable: 40 %, 50 %, 60 % or 70 % of the normal running speed, set by a selector switch. For fastest commissioning, hold the Set/Reset button for 3 seconds: the unit auto-detects and stores the current running speed as the threshold (calibration takes 2–300 seconds depending on speed). No laptop or meter is needed.
Q: Will it false-trip when the conveyor starts up?
A: No. A 20-second start-up delay bypass holds the output until the line reaches steady speed, and the enable terminal is wired to the motor contactor’s auxiliary contact, so the protector only arms once the drive is actually running.
Q: What machines and conveyor types can it protect?
A: Scraper and drag-flight conveyors, bucket elevators (head or foot shaft), slag and ash removal conveyors, and mixers / agitators / kneaders. In short, any shaft-driven machine where a slowdown or stop must cut the drive before secondary damage spreads.
Q: Is it suitable for dusty, wet or hot environments?
A: The speed sensor is IP65 rated and operates from −20 ℃ to 65 ℃ at up to 95 % relative humidity; the controller sits in a rugged industrial housing. It is built for the dust, splash and heat typical of power, cement, grain and wastewater plants.
Q: Do you offer customization, and what is the warranty?
A: Yes — range, output, mounting and cable can be specified for OEM/ODM runs. Send us the machine type, speed and what you need to catch, and we will recommend a configuration. Warranty: free replacement within 15 days for manufacturing defects and free maintenance within 1 year under normal operating conditions (drksir Three Guarantees Policy).